If you work in industries like food processing, packaging, mining, or automotive manufacturing, you know that a conveyor’s performance lives or dies by its components—and few parts are as critical as a perforated steel belt. As a supplier of these belts, I’ve spent years walking alongside maintenance teams, plant managers, and even weekend repair crews through the process of getting a new belt installed correctly. It’s not just about sliding a strip of metal onto rollers; skip a step, and you’re looking off-center tracking, premature wear, or even a dangerous break mid-operation. Today, I’m breaking down the step-by-step process I share with all our customers, drawing on real mistakes I’ve seen (and helped fix) over the years. Perforated Steel Belts
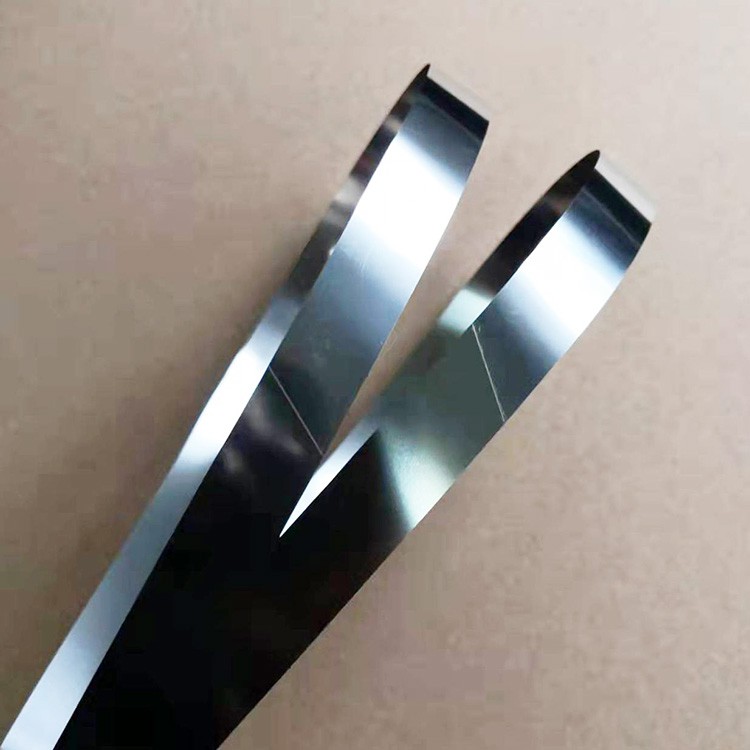
First, a quick pre-installation check that people often skip, and it’s the foundation of a smooth install. Before you even unroll that perforated steel belt, take 30 minutes to inspect your existing conveyor frame, rollers, and drive system. Here’s why: if a roller is bent by even a fraction of an inch, the belt won’t track straight, and all that perforated design—whether it’s for drying bread crumbs, sorting small parts, or draining liquids—will get pulled to one side, leading to uneven material load and extra stress on the belt. I once watched a craft bakery waste $1,200 worth of new perforated steel belts because a technician rushed install and missed a warped return roller. The belt ran off-frame in 48 hours, leading to 12 hours of downtime and a ruined batch of cookies. Save yourself that headache: check every idler roller for straightness, tighten any loose frame bolts, and test the drive motor to make sure it runs at the correct speed (too fast, and the belt will slip; too slow, and you’ll get material buildup in the perforations).
Next, unroll your perforated steel belt properly. This sounds simple, but it’s a detail that trips up first-timers. Perforated steel belts are stiff, so dragging them across concrete or sharp edges will scratch the perforations or bend the metal tabs (for hook-and-loop connections, which are the most common for lightweight to medium-duty belts). The best method is to have two people lift one end of the belt and walk it toward the conveyor, keeping it level the whole time. Don’t unroll it flat on the floor—this can cause the edge to kink, and kinks in steel don’t smooth out easily. If you’re working alone, use a portable roller stand to support the belt as you unroll it, so it doesn’t drag or bend. Also, double-check that you have the right belt orientation: most perforated belts have a “top” and “bottom” side, usually marked with a small notch or a different perforation pattern. The top side is where your material sits, so make sure that’s facing up before you move to the next step.
Now, connecting the belt—this is where the actual work happens, and it’s specific to perforated steel belts. Unlike fabric conveyor belts, perforated steel belts use mechanical connections, most commonly hook-and-loop (also called lacing) or buckle connections, depending on the belt’s thickness. Here, I’ll focus on the two most common types we supply, since they work for 90% of our customers.
For hook-and-loop connections (ideal for 1mm to 3mm thick belts, used in food processing and packaging), start by trimming the ends of the belt perfectly straight. If the ends are uneven, the connection will be weak and cause the belt to stretch unevenly. Use a metal shear or a nibbler—never a hacksaw, which leaves rough edges that can snag on rollers. Once trimmed, lay the two belt ends side by side, overlapping them by 2 to 3 inches (measure twice here—too little overlap and the connection will fail; too much and you’ll have a bump that disrupts material flow). Thread the hook lacing through the perforations: insert one end of the lacing through a perforation on one belt end, then through the matching perforation on the other end, pulling tight until the connection is flat. Use a mallet to tap the lacing down gently, so it doesn’t stick up and interfere with the conveyor’s rollers. I always advise test-fitting the connection before tapping it down all the way—hold the belt up and make sure it lies flat, no gaps between the hook and loop, no excess lacing sticking out.
For buckle connections (used for 4mm to 10mm thick belts, common in mining and heavy manufacturing), the process is a bit different. Buckle connections use two metal plates (one for each belt end) that fasten together. First, punch matching holes through the belt ends using a belt punch tool—make sure the holes line up exactly, otherwise the plates won’t align. Once holes are punched, place the buckle plates on each belt end, align the holes, and insert bolts or rivets (depending on the buckle type) through the holes, tightening them evenly. Again, test the connection: pull gently on the belt to make sure there’s no play in the buckle. A loose buckle is a safety hazard—if it comes loose during operation, the entire belt can shift, causing injury or equipment damage.
Once the connection is in place, it’s time to load the belt onto the conveyor. This is another step where people cut corners. Start by sliding the belt over the head roller (the one connected to the drive motor) first, then work it onto the return rollers and idlers. Keep the belt centered as you go—if it’s even a little off to one side, it will track that way once the conveyor runs. Use a level to check the center line of the belt against the conveyor’s frame, adjusting as needed. Don’t pull the belt tight yet—leave about 1 to 2 inches of slack in the middle, because steel belts expand when they heat up, especially if they’re used for drying or oven applications. Too much tension from the start will cause the belt to stretch over time, leading to premature failure.
Now, the all-important tracking test. A mis-tracked perforated steel belt is not just inefficient—it can damage the belt itself by causing it to rub against the conveyor frame, wearing down the edges of the perforations. To test tracking, start the conveyor at a low speed (10 to 15 feet per minute, not full speed). Watch the belt for 5 minutes—does it stay centered on the rollers, or does it drift left or right? If it drifts, stop the conveyor, and adjust the tracking screws on the idler rollers. Most conveyors have adjustment screws on the side of the idlers that let you tilt them slightly to guide the belt back to center. Adjust one screw at a time, making small tweaks—turning a screw a quarter turn at a time is better than a big adjustment, which can cause the belt to jump off. I once had a mining customer who adjusted the tracking too aggressively in one go, and the belt slipped off, getting caught in the drive system. The fix: small, gradual changes, and frequent checks.
Once the belt is tracking straight, run the conveyor at full speed for 10 more minutes to let the belt settle. Watch for any unusual sounds—grinding, squeaking, or a thumping noise that could indicate a loose connection or a bent belt tab. If you hear anything off, stop and inspect. Common issues here include a loose lacing tab, a roller that’s now showing wear, or a perforation that’s snagging on a bolt. This final check can save you from shutting down production mid-shift later on.
Now, a few pro tips I share with all our customers to keep their perforated steel belts working longer. First, clean the belt regularly—perforations can trap food particles, dust, or debris, which can build up and cause the belt to run unevenly. For food-grade belts, use a mild, food-safe detergent and a soft brush to clean the perforations; never use abrasive scrubbers, which can scratch the metal. For heavy-duty belts, a pressure washer on low pressure works well, but avoid directing water at the drive system or motor. Second, lubricate the rollers periodically—steel belts don’t need special lubrication, but the rollers they run on do. Using a silicone-based lubricant (avoid petroleum-based products, which can attract debris and damage the belt’s finish) will keep the rollers turning smoothly, reducing stress on the belt. Finally, replace small worn parts before they cause big damage—if a roller is bent or a lacing tab is broken, replace that component instead of waiting for the entire belt to fail.
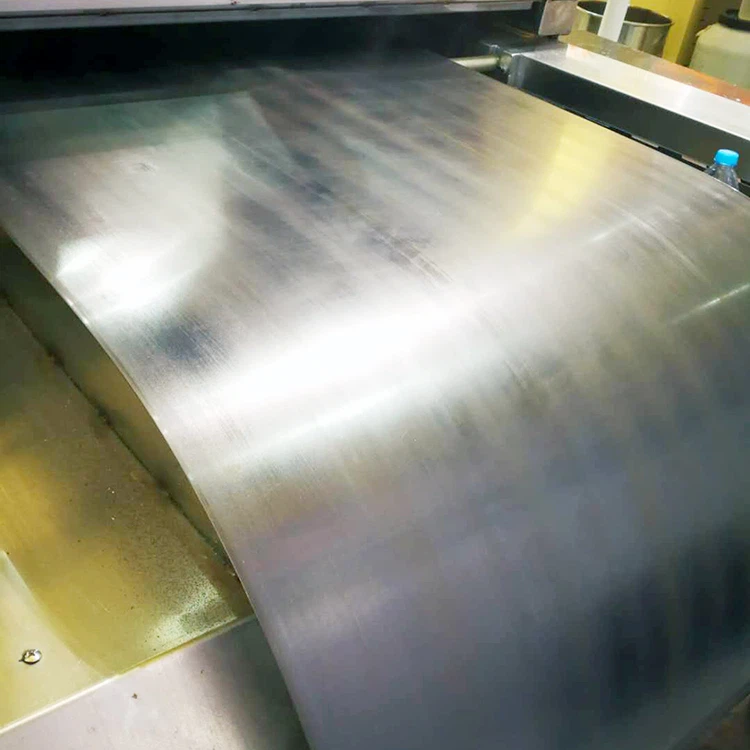
At the end of the day, installing a perforated steel belt is about attention to detail, not just strength. As a supplier, I’ve seen that when customers follow these steps, their belts last 2 to 3 times longer than when they rush the process. If you’re gearing up to install a new perforated steel belt, or if you have questions about troubleshooting a belt that’s not performing as it should, don’t hesitate to reach out. Our team is here to help you select the right belt for your application, walk you through the install, or assist with any maintenance you need.
Endless Steel Belts References:
- Conveyor Equipment Manufacturers Association. "Belt Installation and Maintenance Best Practices." 2022.
- Food and Drug Administration. "Food Processing Equipment: Steel Belt Guidelines." 2021.
- American Society of Mechanical Engineers. "Mechanical Connection Standards for Metal Conveyor Belts." 2020.
Qingdao Acome Machinery Co., Ltd.
Qingdao Acome Machinery Co., Ltd. is one of the most professional perforated steel belts manufacturers and suppliers in China, featured by quality products and good service. Please rest assured to wholesale customized perforated steel belts made in China here from our factory.
Address: No.71-006, YongPing Road, LiCang District, Qingdao, 266041, Shandong Province, China.
E-mail: info@acometech.com
WebSite: https://www.acometech.com/
