If you’ve ever run a heat treat, sintering, or materials testing job with a resistance furnace, you know the struggle: set a temperature, wait hours, and end up with results that are off by 50°C or more. Maybe your ceramic parts have uneven sinter density, or your metal samples don’t meet the hardness specs you need. As a resistance furnace supplier who’s talked to hundreds of foundry, lab, and manufacturing techs over the last 12 years, I’ll tell you—accurate temp control isn’t just about buying a fancy digital controller. It’s a mix of how you set up the furnace, maintain it, and adjust for the stuff no spec sheet tells you. Let’s break this down like I would on a shop floor chat, no boring jargon, just what actually works. Resistance Furnace
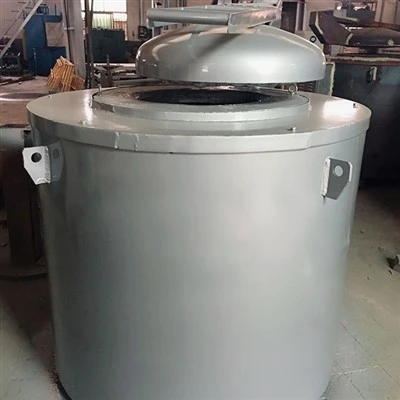
First, let’s get one thing straight: your resistance furnace’s temp reading is only as good as the sensor you’re using. I see so many guys grab a cheap thermocouple, jam it in a random spot, and wonder why their readings are all over the place. Most resistance furnaces use K-type thermocouples for high temps, but even K-types have a shelf life. If yours is more than 18 months old (or if it’s been exposed to corrosive fumes from burnt binders or degreaser), it’s drifting. I had a regular last quarter who swore his furnace was broken—turns out his thermocouple had a cracked sheath, so it was reading 80°C lower than actual in the hot zone. The fix? He swapped it for a grounded, high-temperature K-type, and his sinter yield jumped 20%. Pro tip: Calibrate your thermocouple once every 6 months, not just when your QA guy yells at you. You can grab a cheap calibration kit or send it to a local lab—costs like $50, way cheaper than scrapping a batch of parts.
Then there’s the hot zone. That’s the small area where your parts actually sit, right? A lot of people think “hot zone” is just the center of the heating chamber, but no—resistance furnaces have heating elements (usually wire or rod coils) that lose tension over time, and insulation that compresses. If your heating elements are sagging, they might get too close to the chamber walls, or leave cold spots 2 inches away from the center. I had a customer making dental ceramics who was getting 10°C difference between the left and right trays. We checked his elements—they’d stretched 15% over 3 years, so the right side was only heating to 1550°C instead of the set 1560. We re-tensioned the elements and shimmed the insulation, and the hot zone uniformity dropped to ±3°C. That’s a game-changer for any process where even small temp swings ruin parts.
Now, the controller. This is the brain, and most stock controllers that come with budget furnaces are garbage for precision work. They’re set to “bang-bang” mode, which means the heating elements turn all the way on until they hit the set temp, then cut all the way off. That causes overshoot—your temp might spike 20°C above what you set before it cools down. For things like annealing stainless steel, that’s a big no-no. If you’re running a process that needs tight control (like sintering powder metals or heat treating aerospace parts), you need a PID controller. PID stands for Proportional-Integral-Derivative, and it adjusts the element power smoothly—like a dimmer switch, not a light toggle. You can tweak the gains to match your furnace: if your furnace heats slow, crank up the proportional gain; if it overshoots a lot, turn down the derivative. I often help customers dial these in over a quick call—no need for an engineer, just a few small adjustments on the controller menu.
Wait, but what about the load? That’s another thing no one talks about. If you throw a full tray of cold stainless steel parts into a 1000°C furnace, the temp is gonna drop—hard. A bang-bang controller won’t adjust, so it’ll blast the elements to catch up, then overshoot, and you get a wild swing. The fix here is preheating. If your process lets you, put a small preheat stage at 200°C, then 500°C, before ramping up to your set temp. That way, the load comes up gradually, and the PID controller can adjust power evenly. I also tell customers to never overload the hot zone. If you’re fitting more parts, spread them out so air can circulate around them—blocked airflow is a silent killer of accurate temp. Once, a guy stacked his copper samples so tight that the ones in the middle were 30°C colder than the rest. That’s not a furnace fault—that’s a load fault.
Don’t sleep on the insulation either. If your furnace has old, crumbly insulation, heat leaks out even when the door is closed. I’ve seen furnaces that needed 2 hours to reach set temp, while a well-insulated one takes 45 mins. The heat loss means the controller has to work harder, and it can’t hold a steady temp. If your insulation is more than 5 years old, check for gaps—sometimes the door seal cracks, or the insulation panels pull away from the walls. A quick fix: replace the door gasket (they’re like $30) and fill any small gaps with high-temperature ceramic fiber. That cuts heat loss, makes the furnace respond faster, and keeps the temp steady.
Another common mistake: ignoring process drift. Over time, your furnace’s resistance changes. The heating elements oxidize, so their resistance goes up, meaning they produce less heat for the same voltage. If you’re running the same set point every day, the actual temp might slowly drop—by 10°C a month, until it’s way off. How to fight this? Do a “zone check” once a month. Put a calibrated thermocouple in the center of the hot zone, set the temp, and let it stabilize. If it’s 5°C off, adjust the controller’s offset value. Most PID controllers let you tweak a small offset to match your thermocouple’s reading—no need to change anything else. I had a foundry customer who didn’t do this, and after 8 months, his castings were coming out too soft because the furnace was running 20°C low. A 10-minute zone check fixed that, and he saved thousands in scrapped castings.
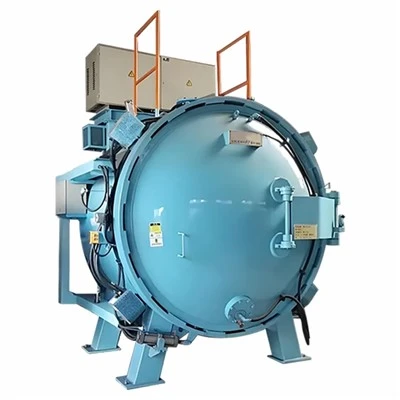
Wait, what about vacuum furnaces? A lot of you might be running vacuum resistance furnaces for brazing or brazing ceramics. Temp control here is trickier because when you pull a vacuum, heat transfer is different—no air to carry heat, so radiation is the main way. If you’re running a vacuum furnace, you need to make sure your thermocouple isn’t sitting too far from the load, because radiation takes time. Also, vacuum pumps can cause small vibrations that might shift a loose thermocouple, so make sure yours is secured tightly. I tell vacuum furnace users to use a shielded thermocouple, too—keeps it from picking up electrical noise from the pump or power lines, which makes readings jump.
Let’s talk about real examples to make this concrete. Last year, a small aerospace parts shop hit me up because their titanium sintering process was failing—their yield was only 65%. They were using a budget 1200°C resistance furnace with a cheap bang-bang controller. We swapped the controller for a PID unit, calibrated their K-type thermocouple, re-tensioned their heating elements, and adjusted their ramp-up profile. After a month, their yield jumped to 98%. That’s not magic—it’s just fixing the small, easy-to-miss issues that throw temp control off.
Now, if you’re running a high-volume process, or one that needs super tight control (like ±2°C or less), there are a few extra steps. First, use a redundant thermocouple. That means two thermocouples in the hot zone, so if one drifts, the controller uses the other. Second, use a chart recorder or a data logger to track temp over time. A lot of new controllers have built-in data logging, so you can see every swing and drift. If you notice a pattern—like every Tuesday at 10 AM the temp drops 15°C—you’ll find it’s because a new batch of parts has more degreaser, which burns off and temporarily cools the chamber. Small issues, but easy to fix once you see them.
And here’s a honest truth I tell every customer: even the best resistance furnace will have temp issues if you don’t use it right. I’ve seen $50k furnaces perform worse than $5k ones just because the operator never calibrates the thermocouple or overloads the hot zone. Conversely, a $5k furnace that’s maintained right can hit ±5°C accuracy, which is enough for most processes.
Now, let’s wrap this up. Accurate temp control isn’t about buying the most expensive gear. It’s: 1) Calibrate your thermocouple every 6 months, 2) Make sure your hot zone is uniform and elements are in good shape, 3) Ditch bang-bang for PID if you need precision, 4) Load your furnace evenly and preheat to avoid temp spikes, 5) Check insulation and gaskets for leaks, 6) Do monthly zone checks to adjust for drift.
If you’re tired of scrapping parts because your temp is off, or your process isn’t meeting spec, I’m here to help. Whether you’re looking to upgrade your controller, replace a worn thermocouple, or even get a custom tune-up for your existing resistance furnace, we can work together to make sure your temp control is as accurate as it needs to be. Just reach out to discuss your needs—no pressure, no sales fluff, just straight talk about what’ll work for your shop.
Tempering Furnace References:
- American Society for Testing and Materials (ASTM) E1441, Standard Practice for Temperature Measurement and Control of Industrial Furnaces
- 2022 Report on Industrial Furnace Efficiency and Temperature Control, International Energy Agency (IEA)
- Thermocouple Maintenance Guide, National Institute of Standards and Technology (NIST) Special Publication 250-87
Danyang Dingfeng Industrial Furnace Co., Ltd.
Danyang Dingfeng Industrial Furnace Co., Ltd. is one of the most experienced resistance furnace manufacturers and suppliers in China, also supports customized service with low price. Please feel free to wholesale high quality resistance furnace made in China here from our factory. For pricelist, contact us now.
Address: Lizhuang Economic Development Zone, Danyang City
E-mail: saleszk@dffurnace.com
WebSite: https://www.dffurnace.com/
