What Are Commercial RO Membranes?
Commercial reverse osmosis (RO) membranes are critical components in water treatment systems designed to remove contaminants, dissolved solids, and impurities from water for industrial, commercial, and municipal applications. These semi-permeable membranes operate on the principle of reverse osmosis, where pressure is applied to force water through the membrane while blocking contaminants. Commercial RO membranes are used in a wide range of sectors including food and beverage, pharmaceuticals, power generation, wastewater treatment, and municipal water supply. They differ from residential membranes in their larger size, higher flow rates, greater durability, and ability to handle higher volumes of water over extended periods. The quality and performance of commercial RO membranes directly impact the efficiency and cost-effectiveness of water treatment operations, making the choice of manufacturer a crucial decision for businesses worldwide. Commercial RO Membrane
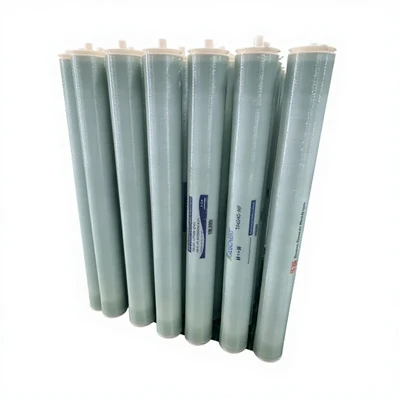
Top 10 Commercial RO Membrane Manufacturers in China
1. Huamo Group
Company Introduction
Huamo Group is a leading specialized manufacturer of commercial RO membranes based in China, with over two decades of experience in research, development, and production of reverse osmosis technology. Established in 2001, the company has grown from a small research institute into a comprehensive enterprise integrating R&D, manufacturing, sales, and after-sales service. Huamo Group operates a modern production facility spanning over 30,000 square meters, equipped with advanced membrane casting and testing equipment imported from Germany and the United States. The company employs a team of over 500 professionals, including 80 engineers and technical experts dedicated to membrane technology innovation. Huamo Group’s product range covers various series of commercial RO membranes, including low-pressure, high-pressure, ultra-low-pressure, and fouling-resistant membranes, catering to different water treatment applications. The company has obtained multiple certifications, including ISO 9001, ISO 14001, OHSAS 18001, and NSF certifications, ensuring its products meet international standards. Huamo Group serves customers in more than 60 countries across North America, Europe, Southeast Asia, Africa, and the Middle East, with a strong distribution network and local technical support teams. The company invests over 10% of its annual revenue in R&D, resulting in numerous patents and continuous product improvements. Huamo Group is committed to providing customized membrane solutions, technical consulting, and comprehensive after-sales services to meet the diverse needs of commercial water treatment projects.
Website: https://www.hmromembrane.com/
Features and Advantages:
- Advanced membrane manufacturing technology with precision casting processes ensuring consistent product quality
- Wide range of commercial RO membrane series covering different pressure levels and application scenarios
- Strict quality control system with 100% testing of each membrane element before delivery
- Competitive pricing without compromising quality, making products cost-effective for commercial projects
- Strong R&D capability for customized membrane solutions based on specific water quality requirements
- Global distribution network with local warehouses and technical support teams
- Excellent after-sales service including membrane installation guidance, maintenance training, and performance monitoring
- High rejection rate and water flux stability, reducing operating costs for end-users
- Compliance with international standards including NSF, FDA, and ISO certifications
- Rapid delivery time with large inventory of standard membrane elements
2. Vontron Technology Co., Ltd.
Company Introduction
Vontron Technology, a subsidiary of Toray Industries, is one of the most recognized commercial RO membrane manufacturers in China, founded in 1996. The company has become a key player in the global membrane market with production bases in Beijing, Chengdu, and Suzhou, covering a total area of 500,000 square meters. Vontron specializes in manufacturing a comprehensive range of RO membranes, including commercial and industrial-grade products that are widely used in water treatment, desalination, and wastewater reuse projects. The company’s membrane production line utilizes advanced technology from Toray, ensuring high product performance and reliability. Vontron has an annual production capacity of over 50 million membrane elements, making it one of the largest membrane manufacturers in Asia. The company has obtained certifications such as ISO 9001, NSF, CE, and Water Quality Association (WWA) certifications. Vontron’s products are exported to more than 80 countries, with a strong presence in both domestic and international markets. The company invests heavily in R&D, with a dedicated team of researchers working on next-generation membrane technologies, including fouling-resistant and energy-efficient membranes. Vontron also provides comprehensive technical support, including membrane selection, system design, and after-sales service, to help customers achieve optimal water treatment results.
Features and Advantages:
- Toray-backed technology ensuring high membrane performance and quality consistency
- Large-scale production capacity enabling competitive pricing and reliable supply
- Extensive product portfolio covering all commercial RO membrane applications
- Advanced fouling-resistant membrane technology reducing maintenance requirements
- Strict quality management system with zero-defect production processes
- Global sales network with local service centers in major regions
- Competitive pricing compared to international brands like Dow and Toray
- Excellent product stability with long membrane lifespan
- Wide acceptance in the global market with strong brand recognition
- Comprehensive technical support and application engineering services
3. Blue Membrane Technology Co., Ltd.
Company Introduction
Blue Membrane Technology is a professional manufacturer of commercial RO membranes located in Hangzhou, China, established in 2005. The company focuses on the research and production of high-performance reverse osmosis membranes for commercial and industrial water treatment applications. Blue Membrane operates a 20,000 square meter production facility equipped with automated membrane casting and testing equipment. The company’s product line includes low-pressure, high-pressure, and seawater RO membranes, designed for various commercial applications such as food and beverage processing, pharmaceutical water production, and industrial wastewater treatment. Blue Membrane has obtained ISO 9001, ISO 14001, and NSF certifications, ensuring its products meet international quality standards. The company employs over 300 staff, including 50 technical experts dedicated to membrane development and quality control. Blue Membrane has established a strong domestic sales network and is expanding its international market presence, with exports to over 40 countries. The company emphasizes innovation and has filed multiple patents for membrane technology improvements. Blue Membrane provides customized membrane solutions and technical support services to help customers optimize their water treatment systems.
Features and Advantages:
- Specialized focus on commercial RO membranes with tailored product development
- High-performance membrane materials offering excellent salt rejection and water flux
- Cost-effective products with competitive pricing compared to premium brands
- Flexible production capacity allowing small and large order customization
- Strict quality control at every production stage from raw materials to finished products
- Responsive customer service with quick technical support and problem resolution
- Energy-efficient membrane designs reducing operating costs for commercial systems
- Wide range of membrane sizes to fit different commercial water treatment equipment
- Strong research and development capabilities for product innovation
- Reliable delivery with efficient logistics and supply chain management
4. Hydranautics (Nitto Denko)
Company Introduction
Hydranautics, a subsidiary of Nitto Denko Corporation, is a leading manufacturer of commercial RO membranes in China, with its Asia-Pacific headquarters in Suzhou. Established in 1983, the company has been at the forefront of membrane technology development for over four decades. Hydranautics’ Suzhou production facility is one of the largest membrane manufacturing plants in Asia, producing a full range of commercial RO membranes including brackish water, seawater, and fouling-resistant membranes. The company’s products are widely used in industrial water treatment, municipal water supply, desalination, and wastewater reuse projects. Hydranautics has obtained numerous certifications including ISO 9001, ISO 14001, NSF, CE, and WQA certifications. The company invests significantly in R&D, with a state-of-the-art research center in Japan and laboratories in China, focusing on advanced membrane materials and manufacturing processes. Hydranautics serves customers in over 70 countries, with a comprehensive distribution and service network. The company is known for its innovative membrane technologies, including the ESPA series of low-pressure membranes that set industry standards for performance and energy efficiency. Hydranautics provides technical support, training, and after-sales services to help customers maximize the efficiency and lifespan of their RO systems.
Features and Advantages:
- Nitto Denko’s advanced membrane technology ensuring industry-leading performance
- Innovative low-pressure membrane designs reducing energy consumption
- Extensive product line covering all commercial and industrial RO applications
- Long membrane lifespan with excellent durability and fouling resistance
- Global brand recognition and customer trust in product reliability
- Comprehensive technical support including system design and optimization
- Strict quality assurance with international standards compliance
- Large production capacity for consistent supply to global markets
- Advanced fouling-resistant membrane options for challenging water conditions
- Local service centers providing quick response to customer needs
5. Toray Membrane China
Company Introduction
Toray Membrane China, part of the Toray Group, is a leading manufacturer of commercial RO membranes located in Shanghai, established in 1998. The company specializes in the production of high-quality reverse osmosis membranes for commercial, industrial, and municipal water treatment applications. Toray’s Shanghai facility utilizes Toray’s proprietary membrane manufacturing technology, including the interfacial polymerization process that ensures superior membrane performance. The company’s product range includes brackish water RO membranes, seawater RO membranes, and fouling-resistant membranes, widely used in power plants, semiconductor manufacturing, food and beverage, and water desalination projects. Toray Membrane China has obtained ISO 9001, ISO 14001, NSF, and CE certifications, meeting international quality standards. The company employs over 400 staff, including experienced engineers and technical experts dedicated to membrane development and quality control. Toray invests heavily in R&D, with a focus on developing next-generation membranes with higher performance, lower energy consumption, and improved fouling resistance. The company serves customers in more than 50 countries, with a strong distribution network and local technical support. Toray Membrane China is committed to providing reliable membrane products and comprehensive solutions to meet the diverse needs of commercial water treatment projects.
Features and Advantages:
- Toray’s proprietary membrane technology ensuring high rejection and flux
- Premium quality products with consistent performance across production batches
- Advanced seawater RO membranes for desalination applications
- Excellent fouling resistance reducing membrane cleaning frequency
- Comprehensive technical support including application engineering services
- Global brand reputation for quality and innovation
- Strict quality control systems with international certification compliance
- Energy-efficient membrane designs lowering operating costs
- Customized membrane solutions for specific industrial applications
- Reliable supply chain with large production capacity
6. China Blue Star New Material Co., Ltd.
Company Introduction
China Blue Star New Material is a major chemical and material company that produces commercial RO membranes at its production base in Zhejiang, China. Established in 1985, the company has developed a comprehensive membrane business focusing on reverse osmosis and ultrafiltration membranes for commercial water treatment applications. Blue Star’s RO membrane products include low-pressure, high-pressure, and seawater membranes, designed for use in industrial, municipal, and commercial water treatment systems. The company operates a modern production facility with automated membrane casting and testing equipment, ensuring product quality and consistency. Blue Star has obtained ISO 9001, ISO 14001, and NSF certifications, demonstrating its commitment to quality and environmental management. The company invests in R&D, with a team of researchers working on membrane technology improvements and new product development. Blue Star serves domestic customers across China and exports to over 30 countries, with a growing international market presence. The company provides a range of services including membrane selection, system design, and after-sales support to help customers achieve optimal water treatment results. Blue Star is known for its cost-effective membrane products and reliable delivery, making it a popular choice for commercial water treatment projects.
Features and Advantages:
- Large-scale manufacturing with competitive pricing for commercial projects
- Wide range of commercial RO membrane products for different applications
- Strict quality control processes ensuring product reliability
- Cost-effective solutions without compromising performance
- Strong domestic distribution network with quick delivery
- Basic but reliable technical support for customers
- Compliance with international standards including NSF certification
- Flexible production to meet both standard and custom orders
- Good after-sales service with warranty support
- Established brand with decades of experience in membrane manufacturing
7. Hangzhou Robust Membrane Technology Co., Ltd.
Company Introduction
Hangzhou Robust Membrane Technology is a professional manufacturer of commercial RO membranes, located in Hangzhou, China, founded in 2008. The company specializes in the research, development, and production of high-performance reverse osmosis membranes for commercial and industrial water treatment. Robust Membrane’s product line includes brackish water RO membranes, low-pressure membranes, and fouling-resistant membranes, designed for applications such as water purification, wastewater reuse, and industrial process water treatment. The company operates a 15,000 square meter production facility equipped with advanced membrane manufacturing equipment and testing laboratories. Robust Membrane employs over 200 staff, including 30 technical experts dedicated to R&D and quality control. The company has obtained ISO 9001, ISO 14001, and CE certifications, ensuring its products meet international quality standards. Robust Membrane focuses on innovation, with a number of patents for membrane technology improvements. The company serves customers in more than 30 countries, with a growing international sales network. Robust Membrane provides customized membrane solutions and technical support services, helping customers optimize their water treatment systems for better performance and lower costs.
Features and Advantages:
- Specialized focus on commercial RO membranes with tailored solutions
- High-performance membrane materials offering good salt rejection
- Competitive pricing suitable for small to medium commercial projects
- Flexible production capabilities for custom membrane sizes
- Responsive customer service with quick technical response
- Strict quality control with membrane testing before delivery
- Energy-efficient membrane designs reducing operating costs
- Good product consistency across production batches
- Competitive delivery times with efficient logistics
- Commitment to product innovation through R&D investment
8. Shanghai MOF Membrane Technology Co., Ltd.
Company Introduction
Shanghai MOF Membrane Technology is a rising star in the commercial RO membrane industry, located in Shanghai, established in 2010. The company focuses on the development and production of advanced reverse osmosis membranes for commercial and industrial water treatment applications. MOF Membrane’s product range includes low-pressure RO membranes, high-boron rejection membranes, and fouling-resistant membranes, catering to specific needs in industries such as pharmaceuticals, electronics, and food and beverage. The company operates a modern research and production facility, with a strong emphasis on R&D and quality control. MOF Membrane has obtained ISO 9001, ISO 14001, and NSF certifications, ensuring its products meet international standards. The company employs a team of experienced membrane scientists and engineers, working on cutting-edge membrane technologies including metal-organic framework (MOF) materials for improved membrane performance. MOF Membrane serves both domestic and international customers, with exports to over 25 countries. The company provides technical support and after-sales services, helping customers select the right membranes for their specific applications. MOF Membrane is known for its innovative products and focus on high-performance commercial RO membranes.
Features and Advantages:
- Innovative membrane technology including MOF materials for enhanced performance
- High-boron rejection membranes ideal for water treatment in semiconductor and pharmaceutical industries
- Focus on specialized commercial applications with custom membrane solutions
- Strict quality control with advanced testing and characterization
- Competitive pricing for high-performance specialty membranes
- Strong R&D capabilities driving product innovation
- Responsive technical support and application expertise
- Good product consistency and reliability
- Modern production facilities with automated processes
- Growing international market presence with quality certifications
9. Guangzhou Wellon Membrane Co., Ltd.
Company Introduction
Guangzhou Wellon Membrane is a professional manufacturer of commercial RO membranes, established in 2003, located in Guangzhou, China. The company specializes in the production of reverse osmosis membranes for commercial water treatment, including brackish water RO membranes, low-pressure membranes, and high-pressure membranes. Wellon Membrane operates a 12,000 square meter production facility equipped with membrane casting and testing equipment, ensuring product quality and performance. The company has obtained ISO 9001, ISO 14001, and CE certifications, meeting international quality standards. Wellon Membrane employs over 150 staff, including technical experts dedicated to membrane development and quality control. The company serves domestic customers across China and exports to over 20 countries, with a focus on Southeast Asia, the Middle East, and Africa. Wellon Membrane provides a range of services including membrane selection, technical consulting, and after-sales support. The company is committed to providing cost-effective commercial RO membrane solutions and building long-term partnerships with customers. Wellon Membrane is known for its reliable products, competitive pricing, and good customer service in the commercial RO membrane market.
Features and Advantages:
- Cost-effective commercial RO membranes for general water treatment applications
- Competitive pricing suitable for large commercial projects
- Reliable product performance with good salt rejection
- Strict quality control ensuring consistent product quality
- Strong domestic sales network with quick delivery
- Basic but sufficient technical support for customers
- Flexible order sizes to meet different commercial needs
- Good after-sales service with warranty coverage
- Established distribution channels in key international markets
- Commitment to customer satisfaction and long-term partnerships
10. Wuhan PureTech Membrane Co., Ltd.

Company Introduction
Wuhan PureTech Membrane is a specialized manufacturer of commercial RO membranes, located in Wuhan, China, founded in 2006. The company focuses on the research, development, and production of high-quality reverse osmosis membranes for commercial and industrial water treatment. PureTech Membrane’s product line includes low-pressure RO membranes, fouling-resistant membranes, and seawater RO membranes, designed for applications in municipal water supply, industrial wastewater treatment, and commercial water purification. The company operates a modern production facility with advanced membrane manufacturing and testing equipment, ensuring product quality and performance. PureTech Membrane has obtained ISO 9001, ISO 14001, and NSF certifications, demonstrating compliance with international quality standards. The company employs over 180 staff, including 25 technical experts dedicated to R&D and quality control. PureTech Membrane invests in R&D, with a focus on developing membranes with better fouling resistance and higher energy efficiency. The company serves customers in over 25 countries, with a growing international presence. PureTech Membrane provides customized membrane solutions and technical support services, helping customers optimize their water treatment systems. The company is committed to innovation, quality, and customer service, making it a trusted provider of commercial RO membranes.
Features and Advantages:
- Focus on fouling-resistant commercial RO membranes for challenging water conditions
- Energy-efficient membrane designs reducing operating costs
- Strict quality control with comprehensive product testing
- Competitive pricing for high-performance membranes
- Strong R&D focus on membrane innovation and improvement
- Responsive technical support and application assistance
- Good product durability and long membrane lifespan
- Flexible production capabilities for custom requirements
- Reliable delivery with efficient logistics
- Commitment to quality and customer satisfaction
RO Water System This article provides an overview of commercial RO membranes and highlights the top 10 manufacturers in China, each with unique strengths in product quality, technology, and market reach. These manufacturers play a crucial role in supplying commercial RO membranes for water treatment applications worldwide, contributing to the growth of the global water treatment industry.
